Premium Ceramic Crucibles | High-Performance Lab & Industrial Solutions

Key takeaways
- Boron nitride crucibles with excellent machinability allow fabrication of complex shapes (thin walls, threads, undercuts) using conventional machining.
- The layered hexagonal structure and low hardness (Mohs 1–2) enable carbide or HSS tooling without diamond grinding.
- Machinable BN crucibles reduce lead time and tooling cost for custom or prototype geometries.
- Key applications include III-V semiconductor crystal growth, reactive metal melting, and laboratory thermal analysis.
- Maximum service temperature is approximately 1800°C in inert atmosphere; binder selection affects purity and thermal shock resistance.
What Is a Boron Nitride Crucible with Excellent Machinability?
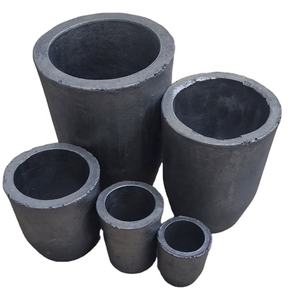
A boron nitride crucible with excellent machinability is a ceramic crucible made from hexagonal boron nitride (h-BN) that can be precisely shaped and machined into complex geometries using standard tooling. Unlike many high-temperature ceramics such as a reaction sintered silicon nitride crucible that require near-net-shape forming, BN crucibles can be turned, milled, drilled, and threaded after densification, enabling tight tolerances and intricate internal or external features that are difficult to achieve with other refractory materials.
'Excellent machinability' means that the material behaves similarly to a soft metal or graphite during cutting, allowing manufacturers to produce thin walls, undercuts, threaded sections, or multi-cavity designs without post-firing or diamond tooling. This property is particularly valuable when the crucible shape must match a specific heating profile, accommodate a non-standard charge, or fit into a confined space in vacuum or inert-gas furnaces.
A boron nitride crucible with excellent machinability is defined both by its chemical composition (typically hot-pressed BN with a binder system) and by the ability to economically produce small batches or one-off complex designs that would be prohibitive with castable or pressed-and-sintered ceramics.
Key Material Properties That Enable Machinability
The machinability of boron nitride crucibles stems from the layered crystal structure of hexagonal BN, similar to graphite but with different interlayer bonding. This structure provides low hardness on the Mohs scale (typically 1–2) and low fracture toughness, allowing chips to form cleanly during cutting without catastrophic cracking. In contrast, a hot pressed silicon nitride crucible, despite its high strength at elevated temperatures, requires diamond grinding because of its high hardness.
Unlike alumina or silicon nitride, which require diamond grinding for material removal, BN can be machined with carbide or even high-speed steel tools. The material also exhibits self-lubricating characteristics due to its platelet morphology, reducing tool wear and enabling high cutting speeds and fine surface finishes.
Hot-pressed BN grades used for crucibles are typically densified to 90–98% of theoretical density using a binder such as boron oxide or calcium borate. These binders improve the green strength and thermal shock resistance while maintaining machinability. The resulting material has a flexural strength of 40–80 MPa and a compressive strength of 100–200 MPa, sufficient for handling and thermal cycling when properly designed.
| Property | Description |
|---|---|
| Crystal Structure | Hexagonal layered structure similar to graphite; provides low hardness and self-lubrication |
| Hardness | Mohs 1–2; can be machined with carbide or HSS tools |
| Thermal Conductivity | High in-plane (≈30–60 W/m·K) enabling fast heat transfer |
| Maximum Service Temperature | Up to 1800°C in inert atmosphere; lower in vacuum or oxidizing conditions |
| Chemical Resistance | Inert to most molten metals, glasses, and salts; non-wetting to many melts |
| Typical Binder | Boron oxide or calcium borate; enhances density and thermal shock resistance |
How Machinability Enables Complex Shapes in Crucibles
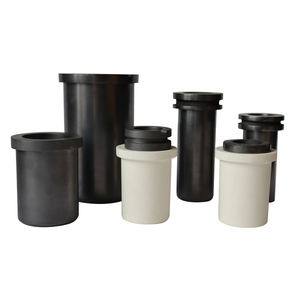
Excellent machinability expands the range of achievable shapes for BN crucibles. Complex features such as thin fins for heat transfer, stepped inner diameters for nesting components, and passages for thermocouples or gas lines can be easily produced by conventional CNC or manual machining.
For example, a crucible intended for molecular beam epitaxy (MBE) may require a conical interior with multiple baffles to control vapor distribution. Such a shape would be extremely difficult to press or cast but can be machined from a single BN billet. Similarly, custom chutes, boats, and liners for powder handling can be produced with square pockets or dovetail slots.
The ability to machine complex shapes also reduces lead time. Instead of waiting weeks for a custom die or mold, a machinist can produce a prototype or short-run component in days. This agility is critical in research and development environments where crucible geometry often evolves during experimentation.
Typical Applications Requiring Complex BN Crucibles
BN crucibles with excellent machinability are used in processes where high purity, thermal stability, and non-wetting behavior are essential. They are common in the growth of III-V semiconductors (e.g., GaAs, InP) where the crucible must withstand molten gallium or indium without contamination. Complex shapes like conical nozzles or multiple-baffle configurations are often required to control evaporation rates.
In the metallurgical sector, BN crucibles serve as containers for melting reactive metals such as aluminum, copper, and zinc alloys. Machinable grades allow fabricators to add pouring lips, handles, or indexing features directly to the crucible body, improving handling and pouring accuracy. For semiconductor wafer processing, a silicon nitride crucible provides excellent purity but lacks the machinability of BN for adding custom features.
Research laboratories rely on custom-machined BN components for thermogravimetric analysis (TGA) and differential scanning calorimetry (DSC), where sample pans and crucibles must have exact internal volumes and thin walls to ensure uniform heating. The machinability of BN permits very small (milliliter-scale) or very thin-walled (<1 mm) designs that would be impossible with pressed ceramics.
Summary: Key Advantages of a Machinable BN Crucible
The core advantage of a boron nitride crucible with excellent machinability is design freedom. Users are not limited to standard catalog shapes; they can specify geometries that optimize thermal profiles, material flow, or equipment fit. This is especially important when upgrading existing furnaces or building custom deposition systems.
From a production standpoint, the machinability reduces tooling costs, shortens lead times, and allows for iterative design improvements without the expense of new dies. The trade-off is that machinable BN grades may have slightly lower maximum service temperatures (typically up to 1800°C in inert atmospheres, compared to 2000°C+ for pure, binderless BN) and may require careful handling to avoid edge chipping during machining.
When selecting a BN crucible, the decision should balance the need for complex geometry against the temperature and purity requirements of the process. For applications where intricate shapes are mandatory, a machine-grade BN crucible offers a practical, economical solution.
Frequently asked questions
What is the difference between machinable BN and standard BN crucibles?
Machinable BN crucibles are specifically formulated with a binder system that allows post-sintering machining using conventional tools. Standard BN crucibles may be pressed or isostatically pressed into near-net shapes and then sintered, but they are not designed for extensive machining. Machinable grades offer greater design flexibility but may have slightly lower purity and maximum temperature ratings.
Can a machinable BN crucible be used in vacuum?
Yes, but the maximum safe operating temperature is lower in vacuum than in inert gas. Typical BN compositions can be used in vacuum up to about 1200–1400°C, depending on the binder content. At higher temperatures, decomposition and loss of binder may occur. Check the manufacturer's data sheet for specific limits.
How small can I machine a complex feature in a BN crucible?
Feature size depends on the tool capability and the fragility of the BN. Thin walls down to 0.5 mm, small holes down to 1 mm diameter, and threads as fine as M3 can be reliably machined. Finer features are possible with careful handling, but edge chipping risk increases.
Do I need special cooling or lubricant when machining BN?
No. BN can be machined dry or with a mild air blast to clear chips. Coolants are generally not required and may introduce contamination; if used, avoid water-based fluids that could hydrolyze the binder. Graphite or molybdenum disulfide lubricants can help with tapping.
.